Factory & Quality & About
A trusted candy manufacturer with 15+ years of experience serving global brands
Our Story
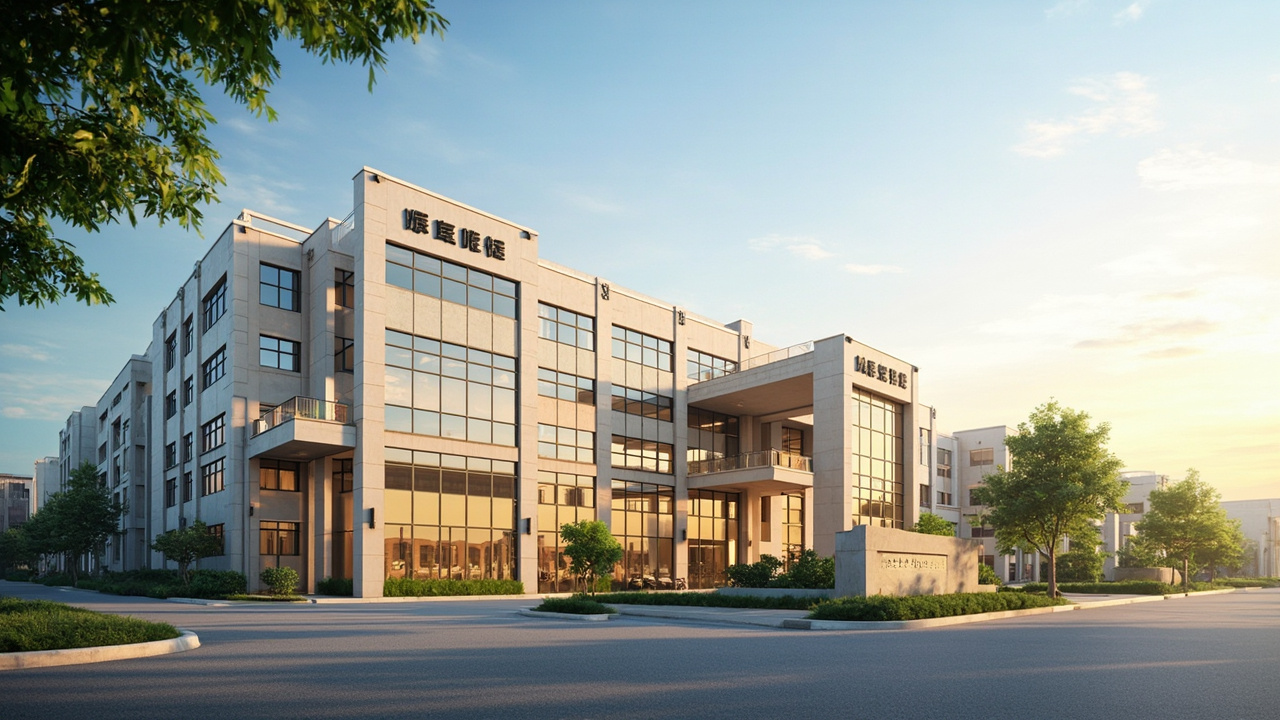
Founded in 2008, our candy factory has grown from a local manufacturer to a trusted OEM partner for brands worldwide. We specialize in gummy candy, hard candy, aerated candy, toffee, and compound chocolate products.
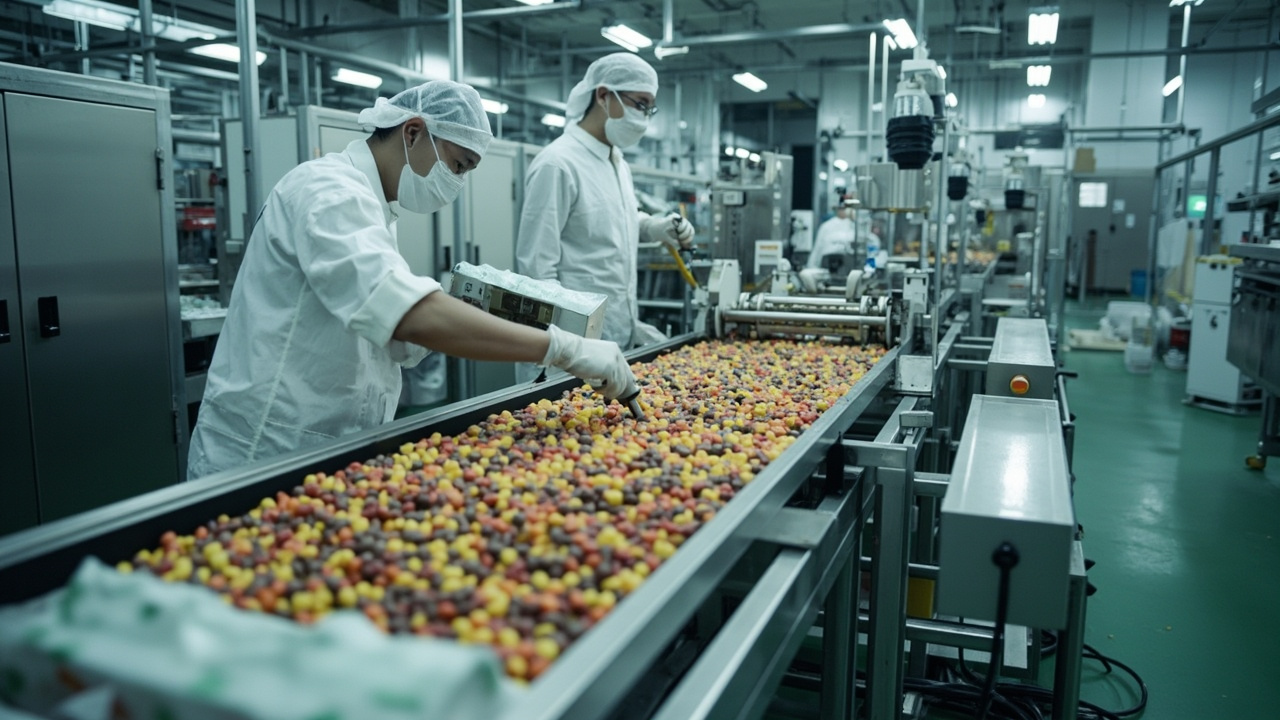
Our facility spans 20,000 square meters and is equipped with state-of-the-art production lines capable of producing 100 tons of candy daily. We serve clients across Europe, North America, Southeast Asia, and the Middle East.
Quality Control
Comprehensive quality management at every stage
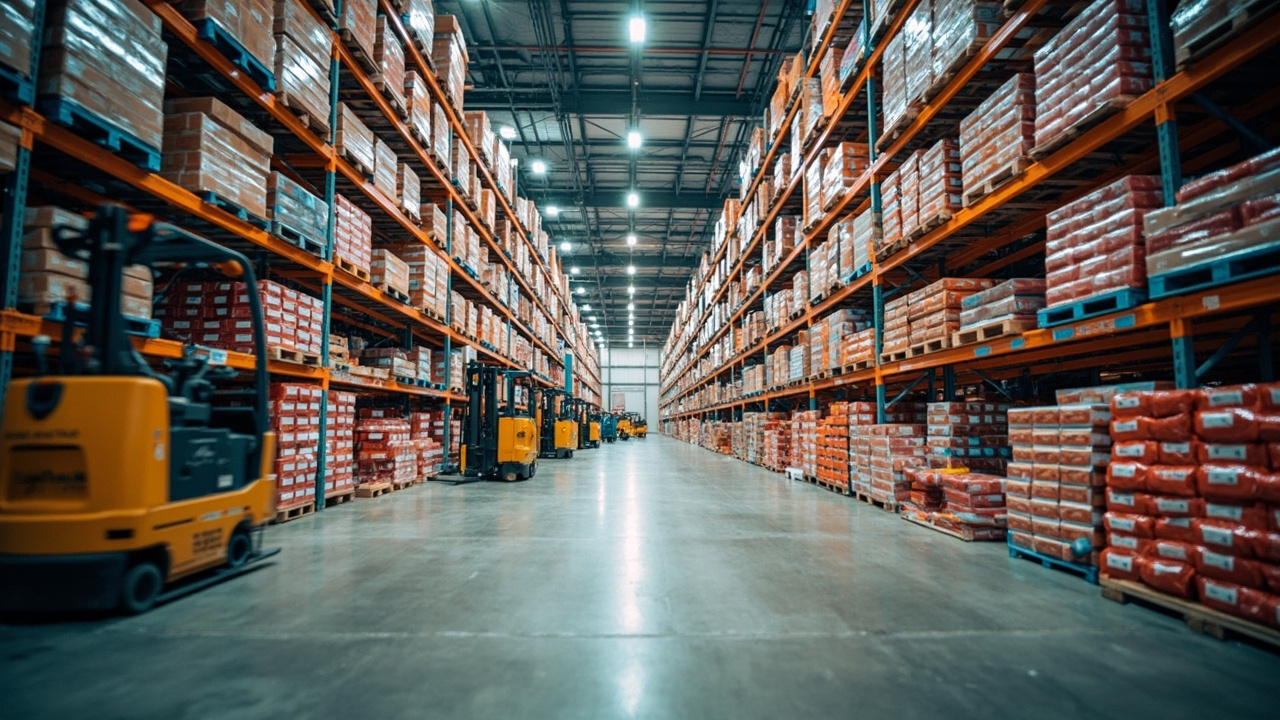
Raw Material Testing
All incoming materials are tested before use
- Supplier qualification audit
- Certificate of analysis verification
- Microbiological testing
- Physical & chemical analysis
In-Process Control
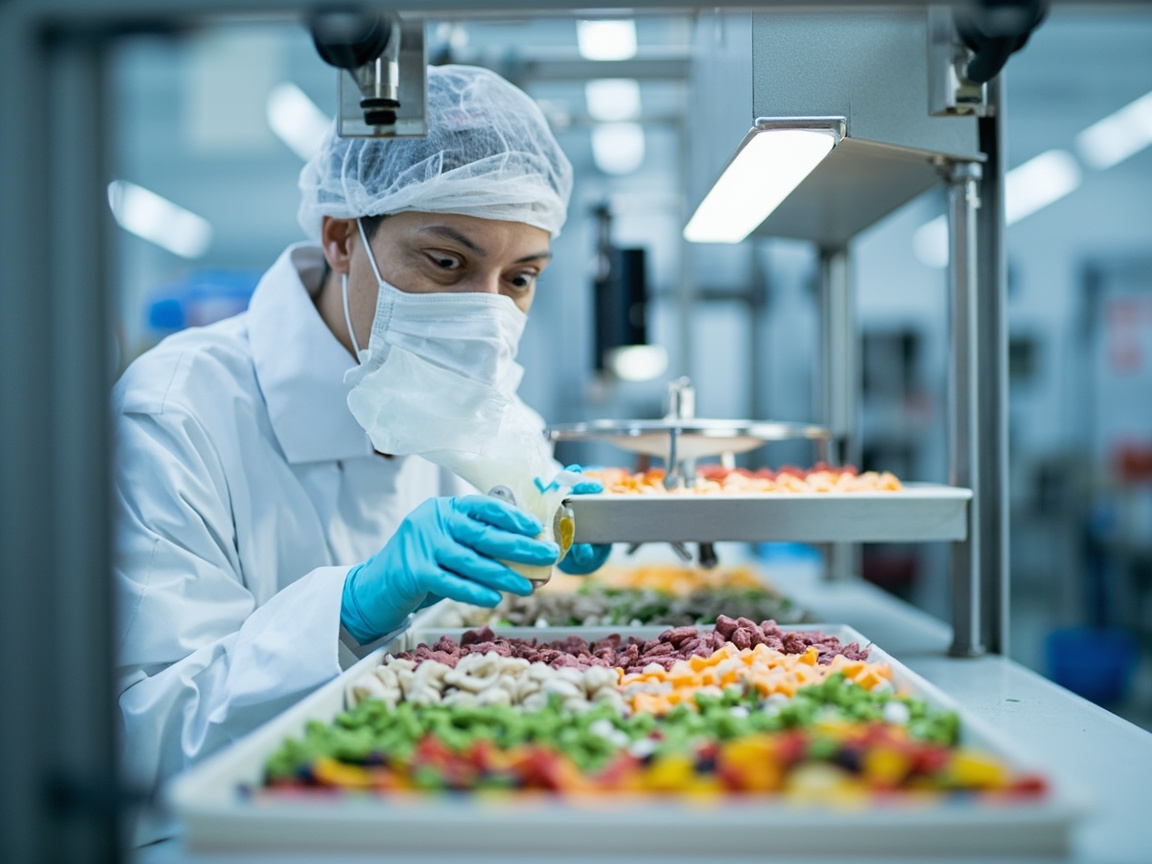
Real-time monitoring during production
- Temperature monitoring
- Metal detection
- Weight control checks
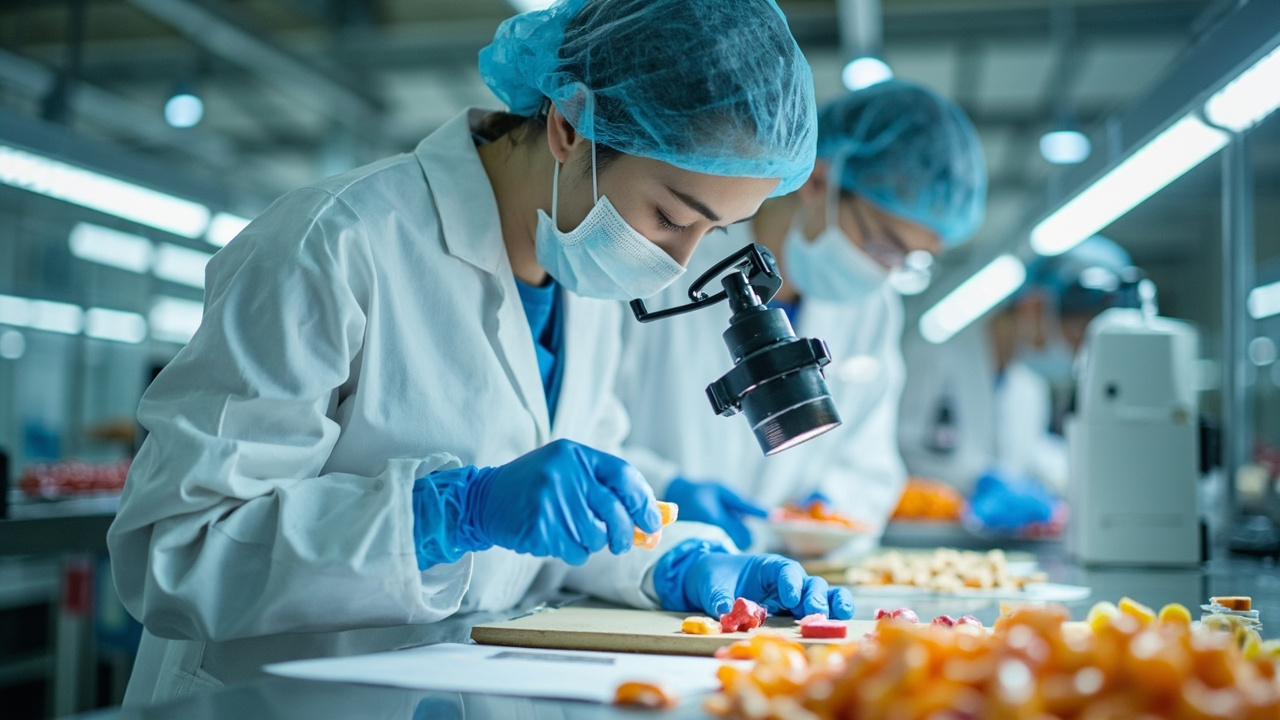
- Visual inspection every 30 minutes
Finished Product Testing
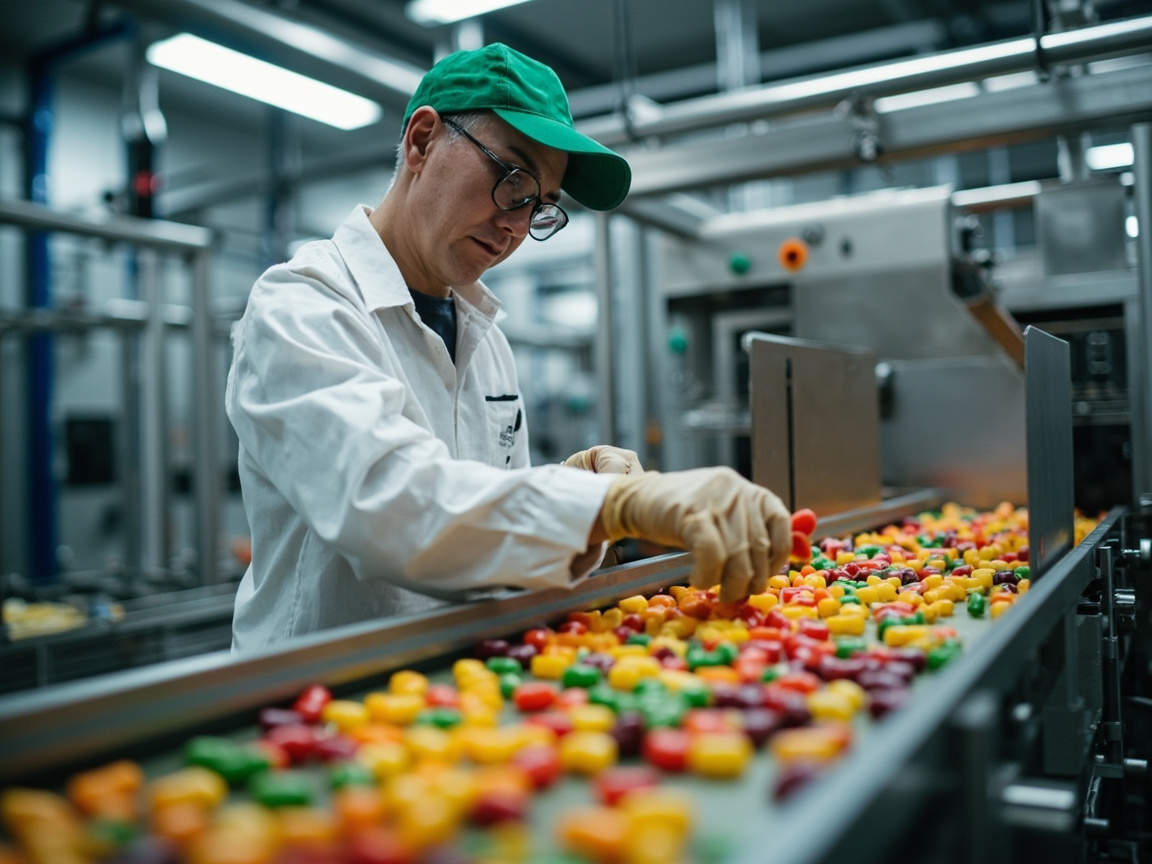
Comprehensive testing before release
- Sensory evaluation
- Microbiological testing
- Package integrity testing
- Shelf life verification
Traceability System
Complete traceability from raw materials to finished products
Raw Material
Verified & recorded upon receipt
Production
Batch tracking throughout process
Packaging
Batch codes printed on each package
Shipping
Full traceability to customer
Batch Tracking
Each batch assigned unique identifier for full traceability
Sample Retention
Production samples retained for 24 months for quality reference
Documentation
Complete production and testing records for every batch
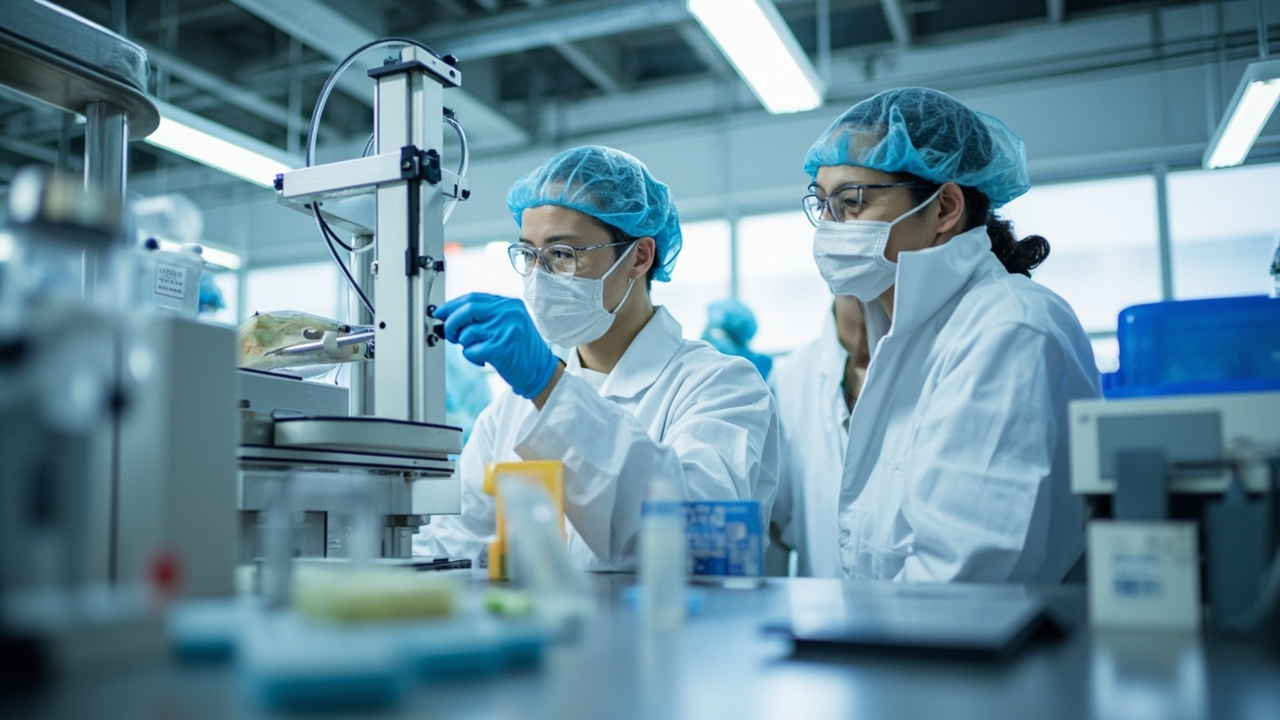
Laboratory Testing
On-site laboratory equipped with advanced testing equipment
- Microbiological Testing
Bacterial count, yeast & mold analysis
- Chemical Analysis
Composition, moisture content, pH testing
- Physical Testing
Texture, hardness, color measurement
- Third-Party Labs
SGS, Intertek, BV for export certification
Quality Milestones
Our journey in quality excellence
Factory Founded
Established with 2 production lines
First Export
Started exporting to Southeast Asia
HACCP Certification
Achieved HACCP food safety certification
Expansion
Expanded to 20,000 sqm facility
ISO 22000 & BRC
Added ISO 22000 and BRC Grade A certifications
New Production Lines
Added 4 more automated production lines
Documents & Certificates
Send Inquiry
Visit Our Factory
We welcome clients to visit our facility and see our quality processes firsthand